01 · On-site video
Clutch Cover Assembly Line
Clutch covers are assembled and checked at each workstation.
 Get Quote
Quality control
Incoming material, dimensional, applicable performance and final checks for truck-parts orders, including labels and export packing.
Inspection at the factory
Checks are selected against the part drawing and order requirements.
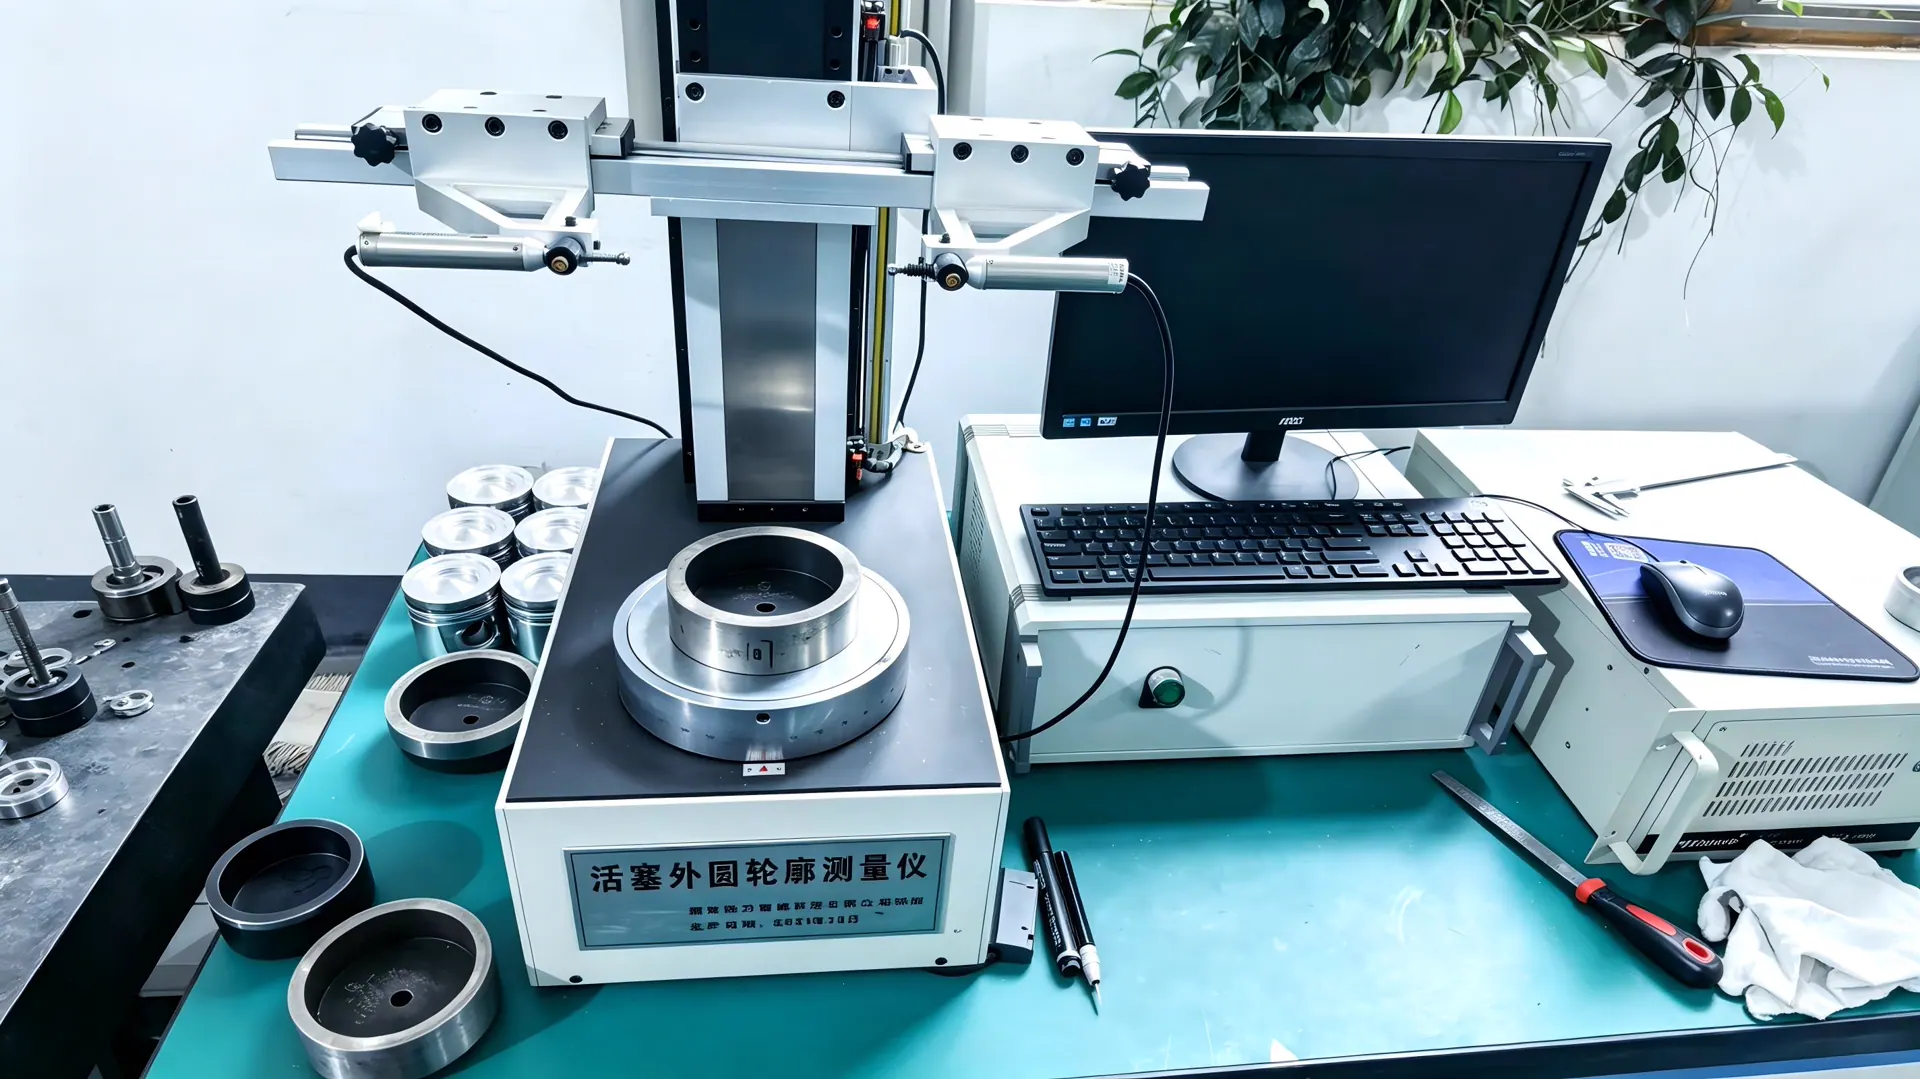
The measuring station shown is used to check piston outer profiles. The piston reference and drawing define the dimensions to inspect.
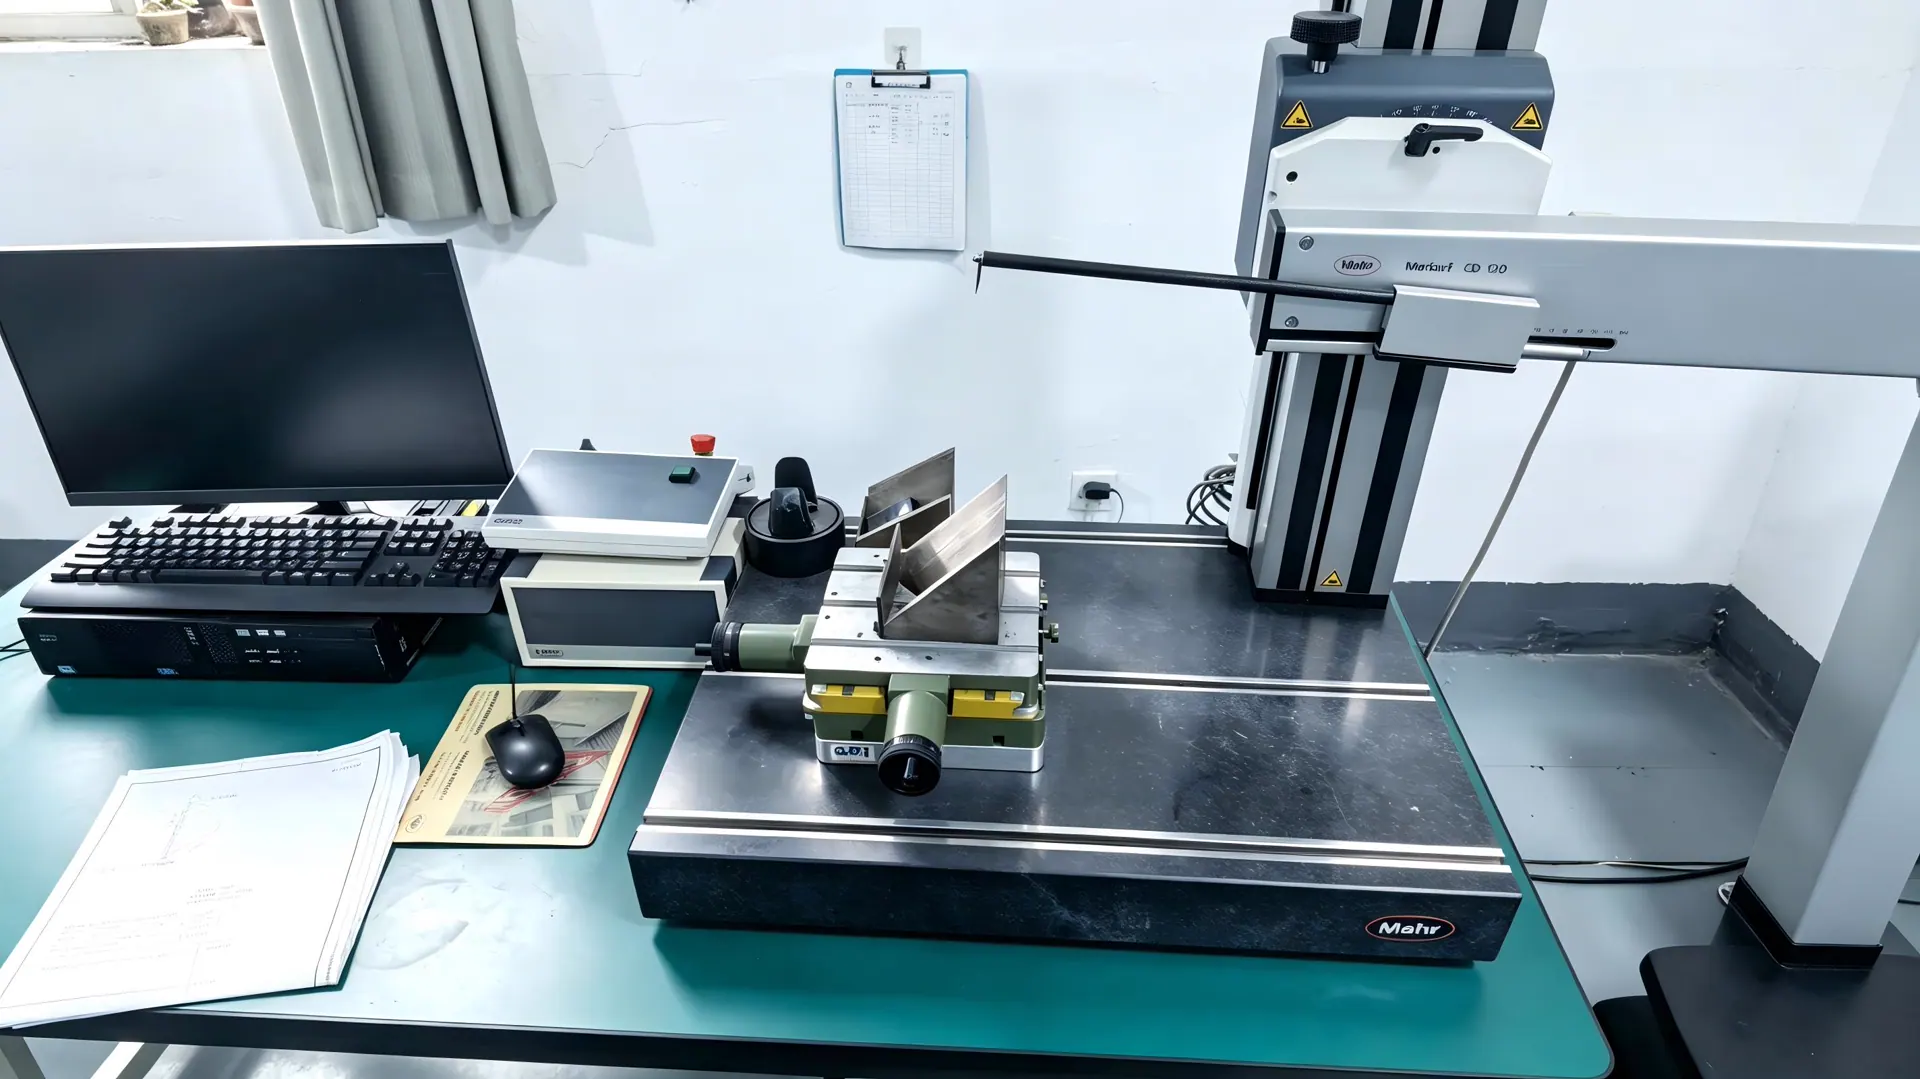
A probe and fixture are used to measure a component profile. The workpiece, measurement path and acceptance limits are selected for the particular part.
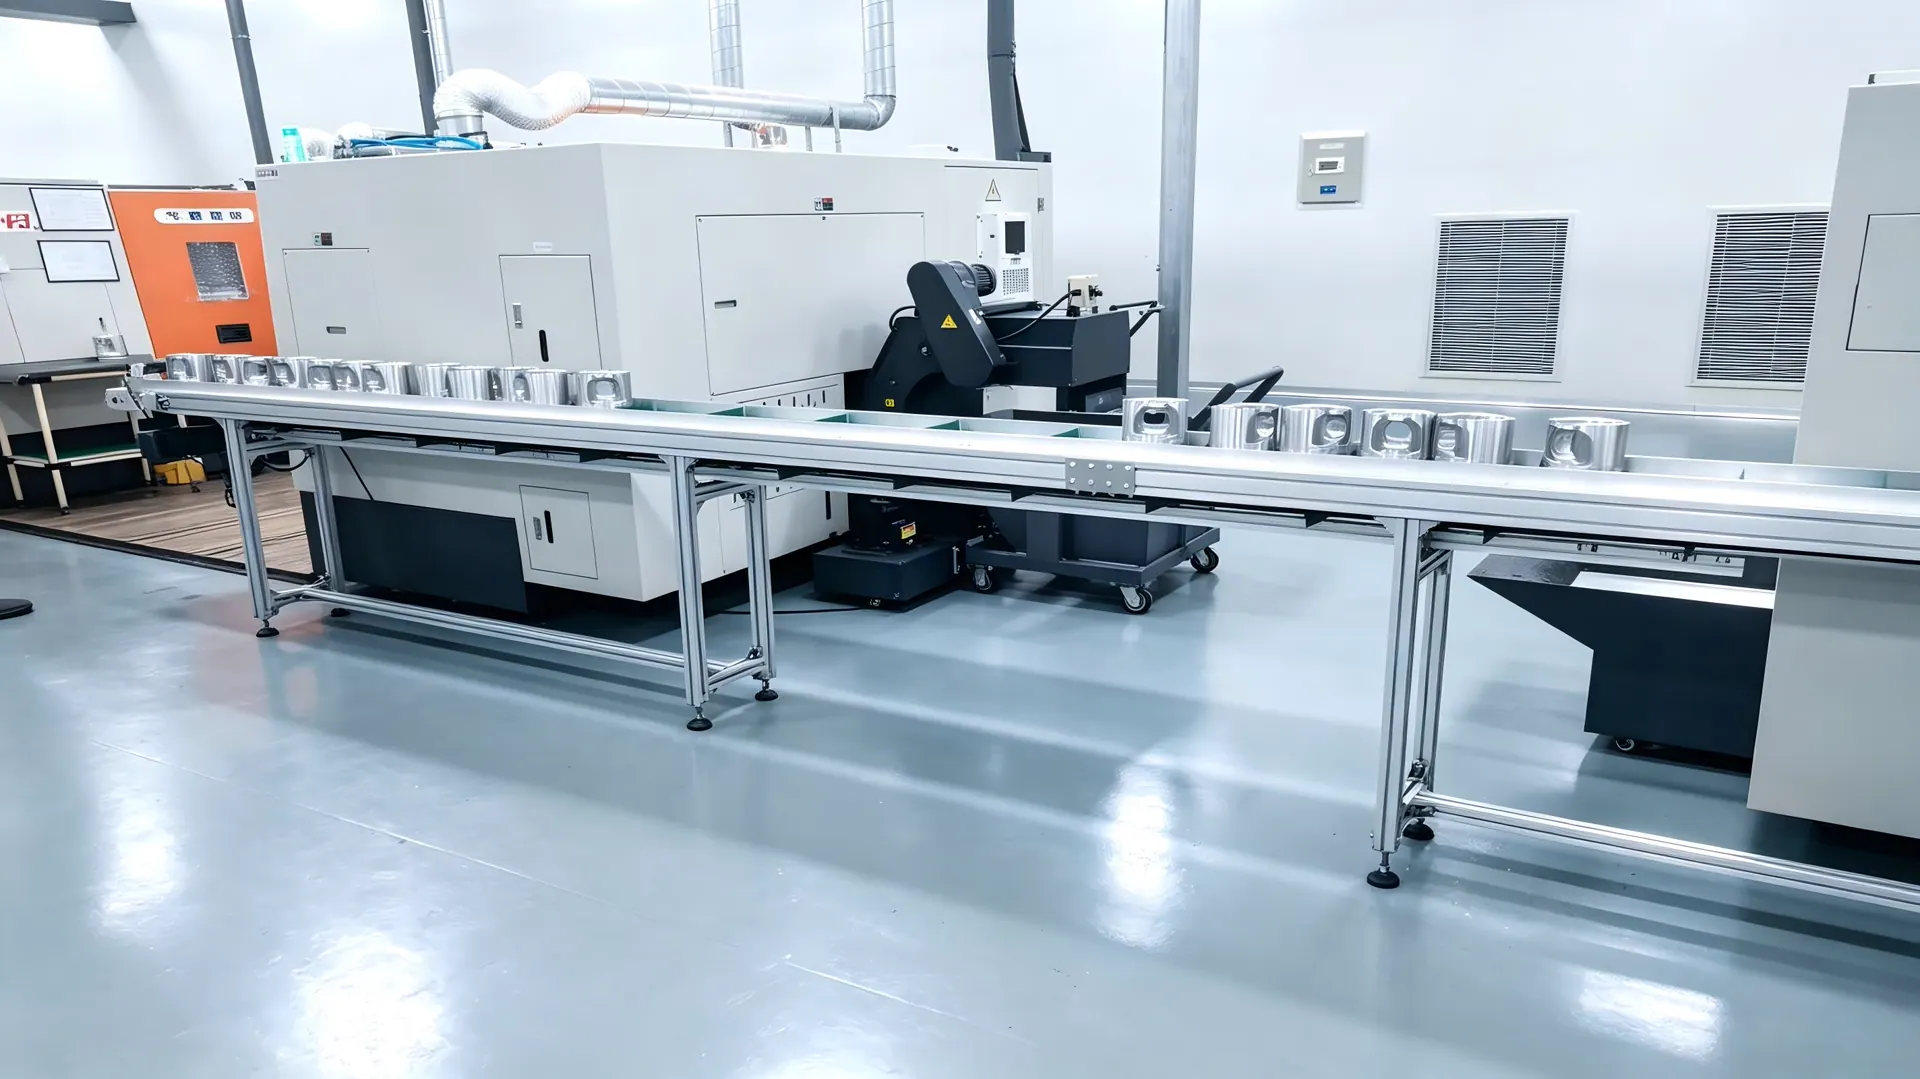
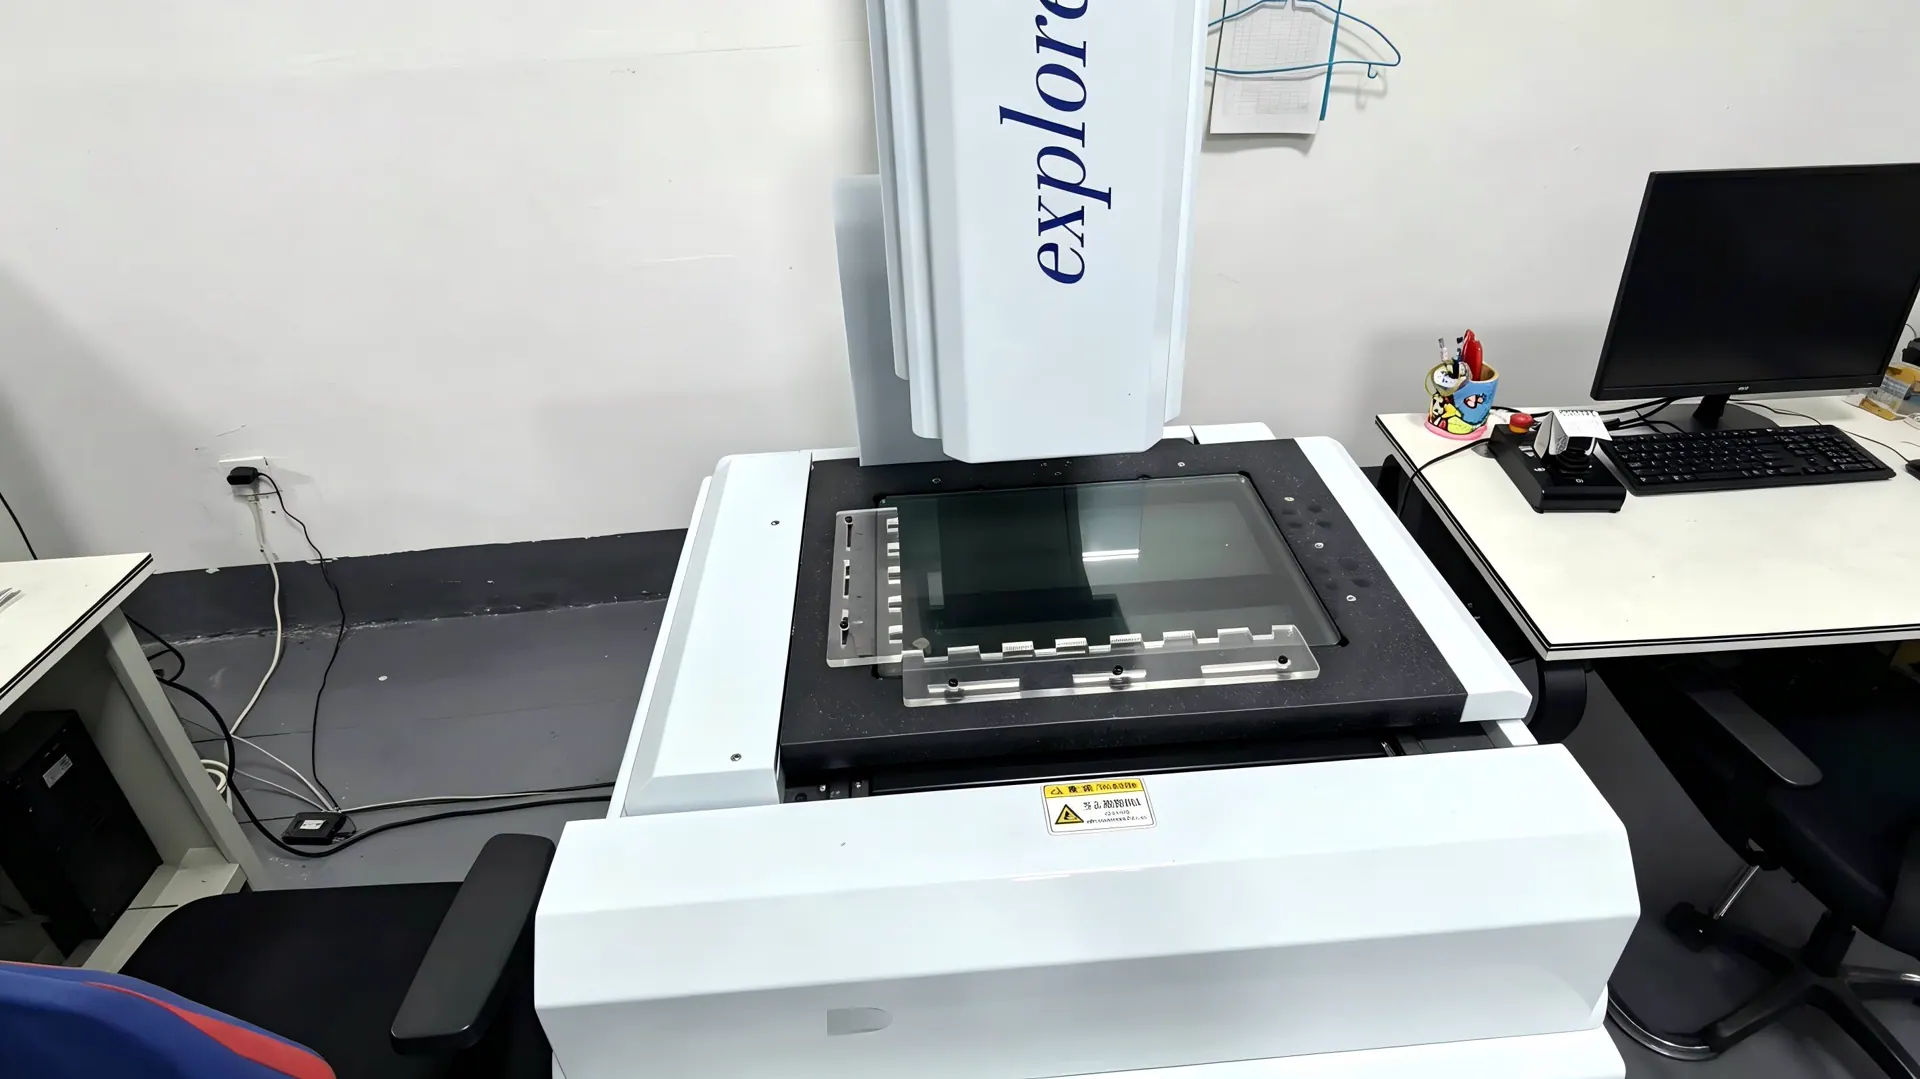
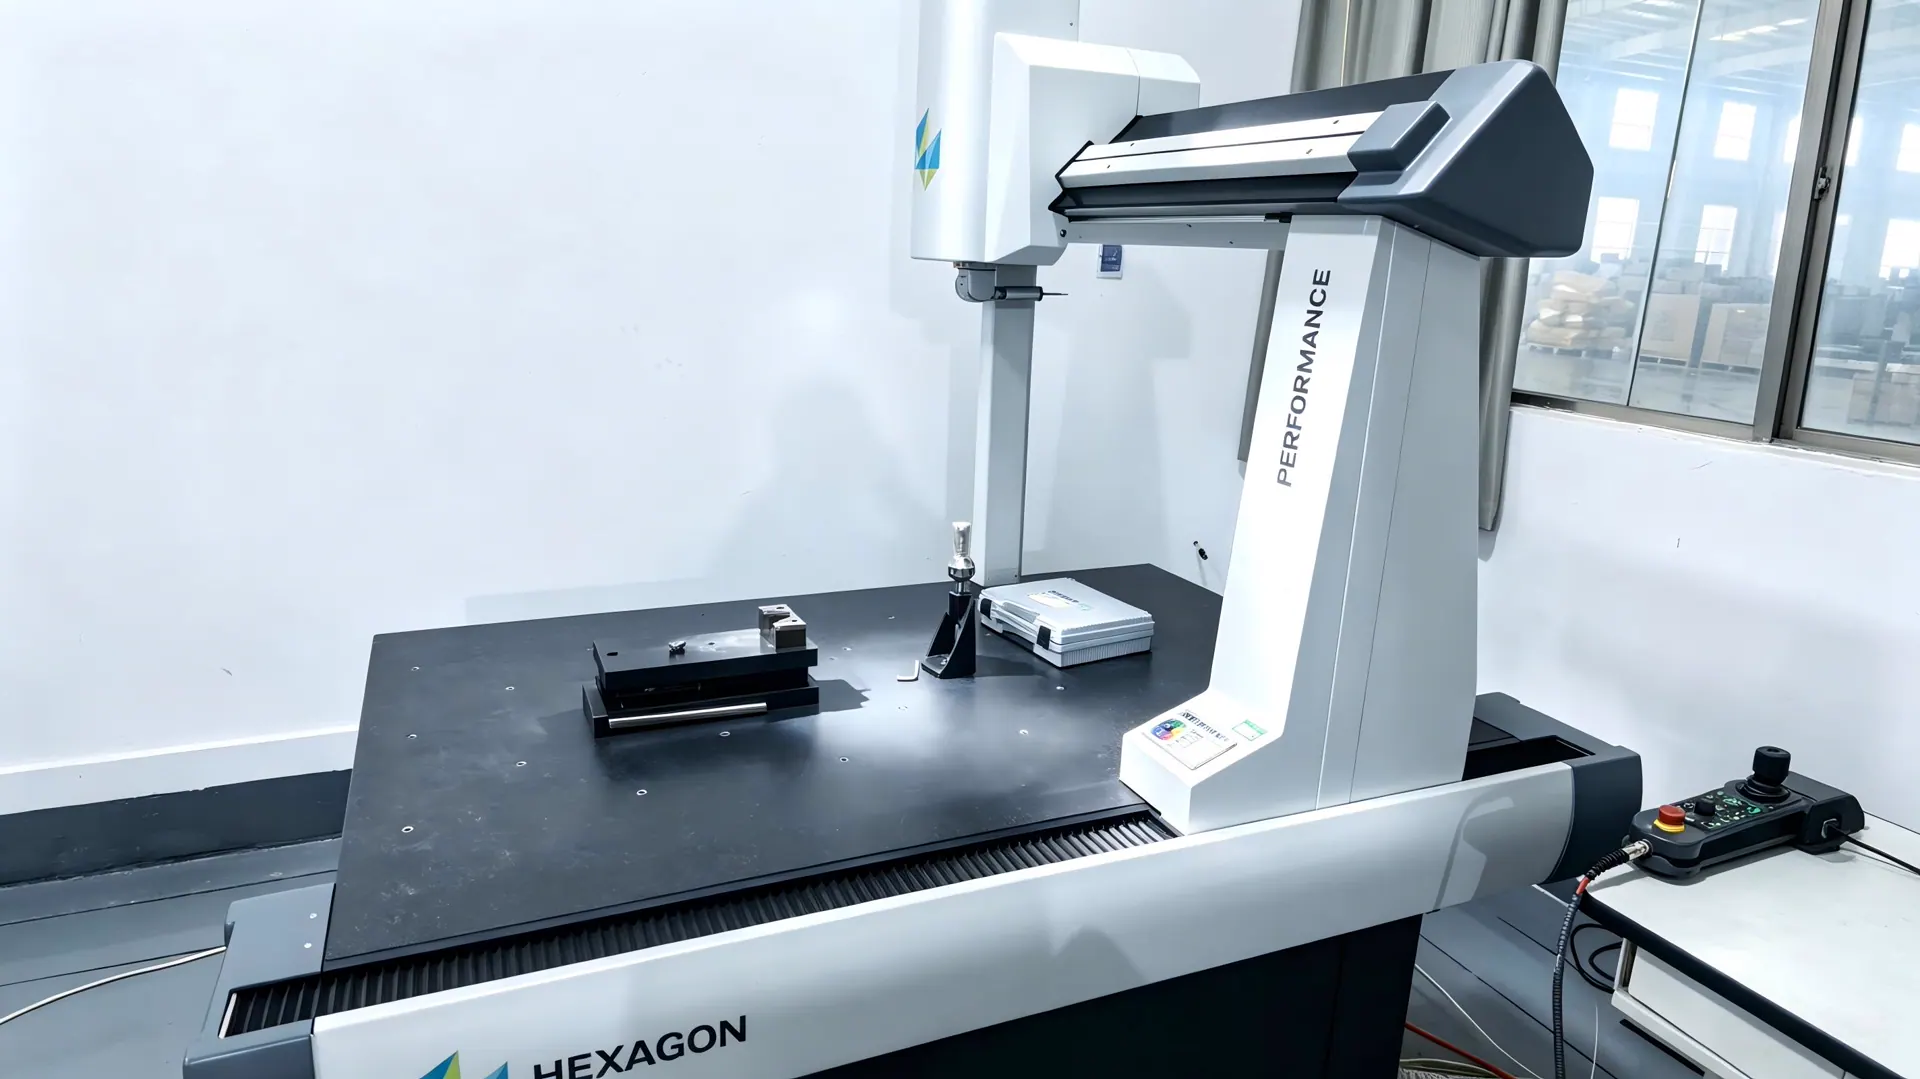
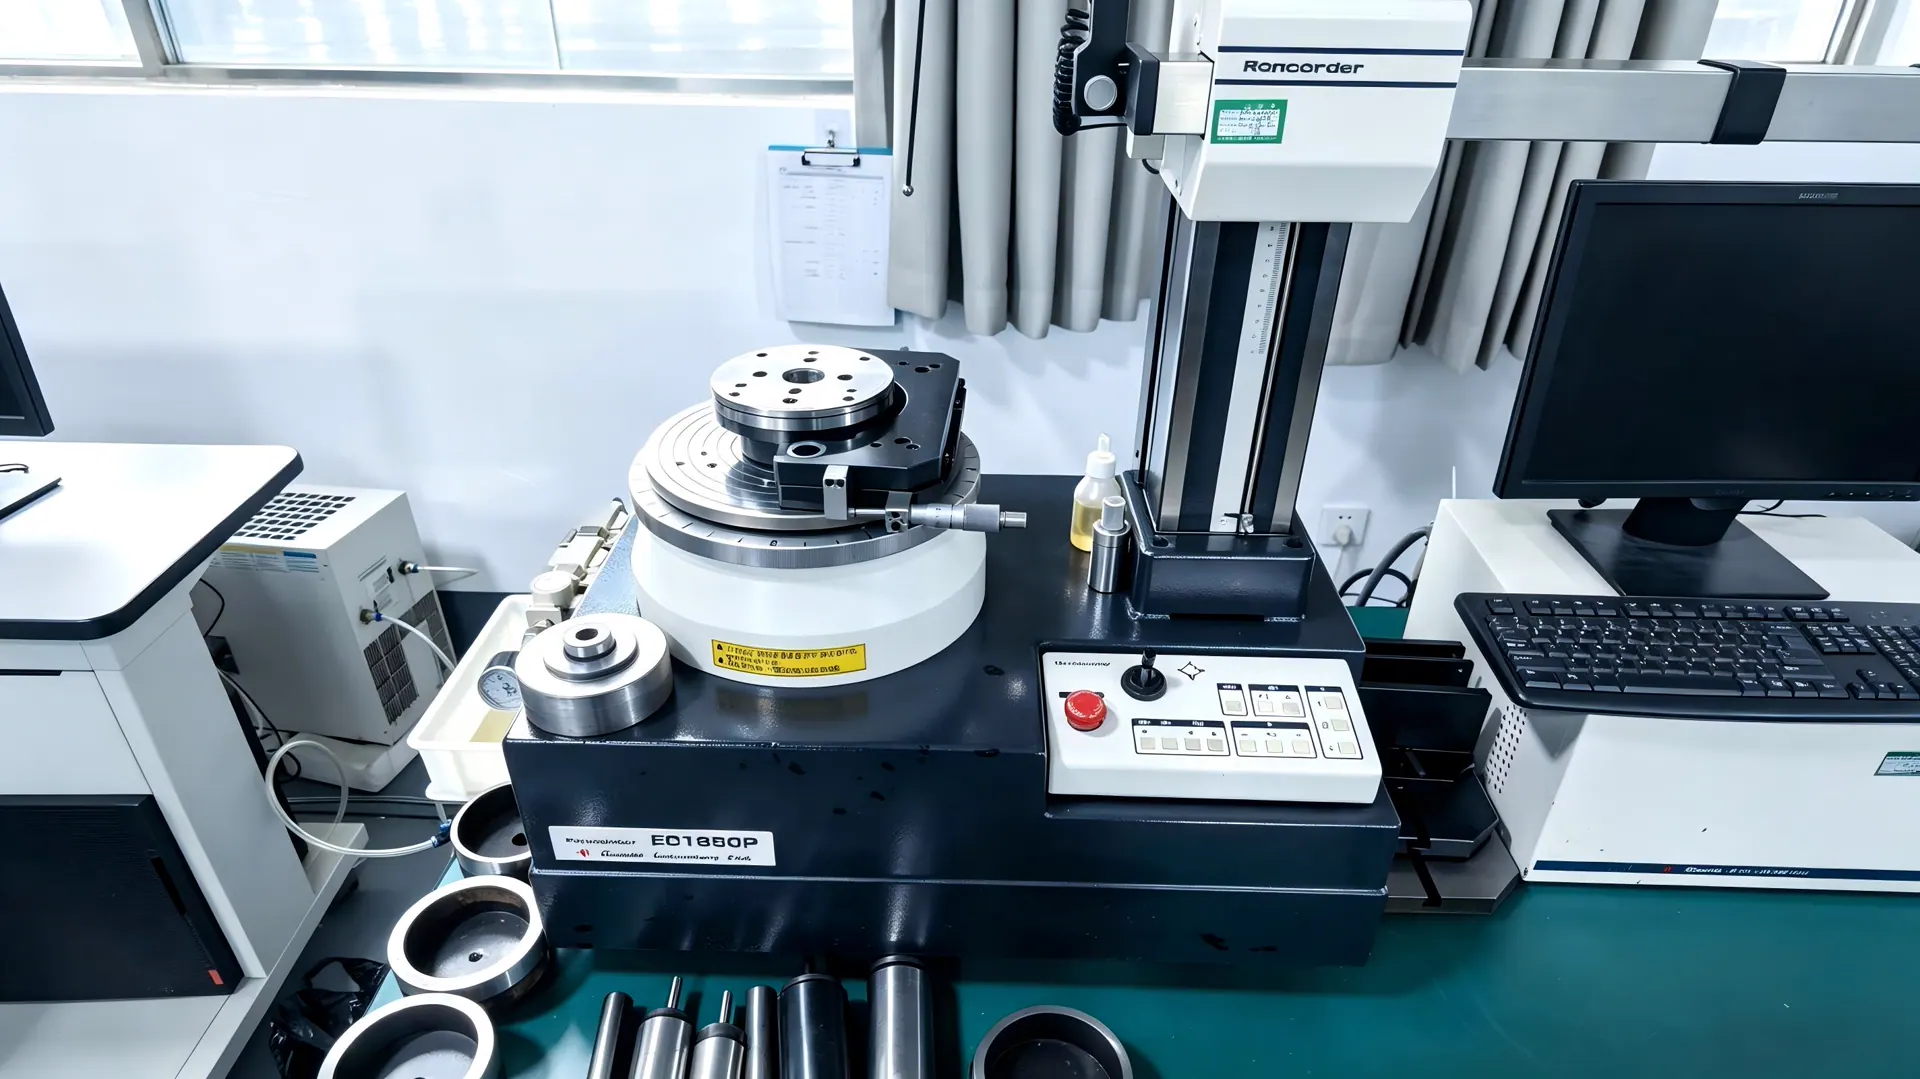
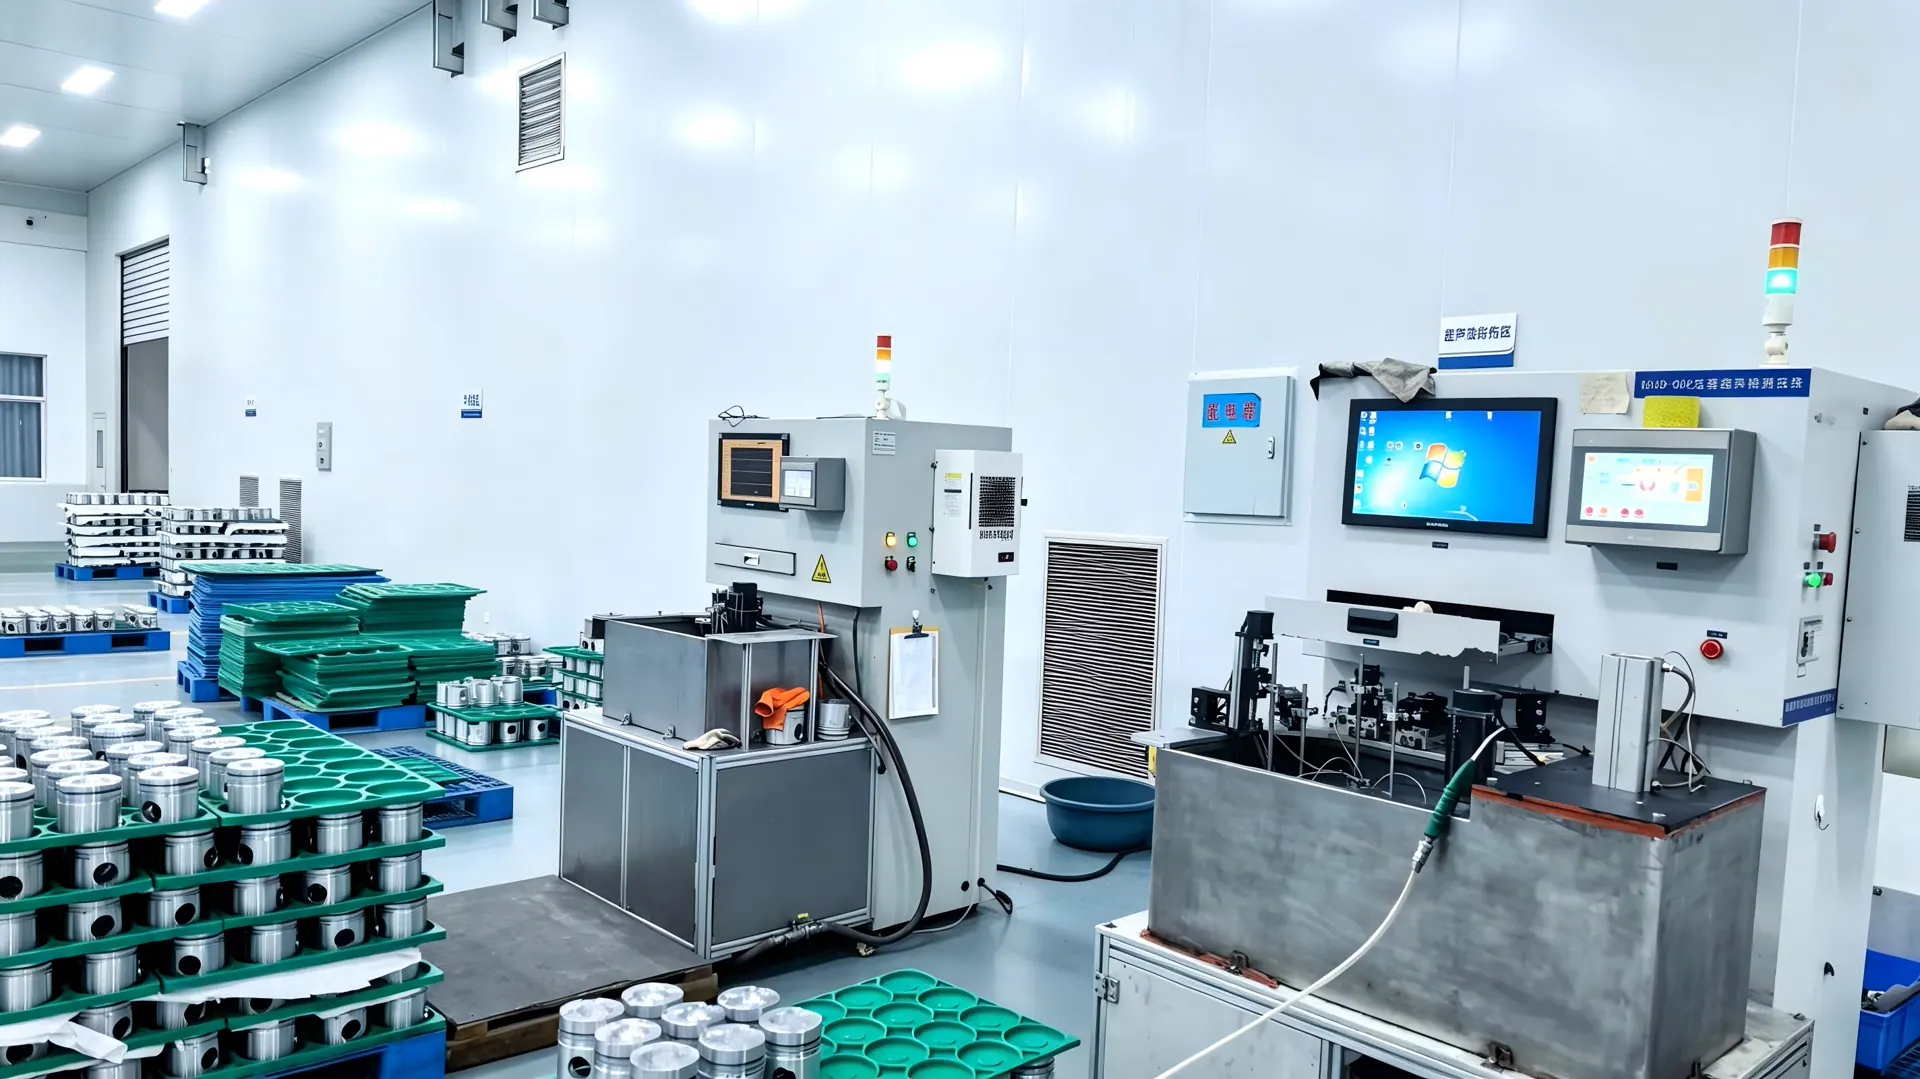
Incoming inspection checks whether the received material or component matches the approved purchase reference before it enters production or packing.
View details02Dimensional inspection focuses on the features that determine fit, sealing, alignment or connection with neighboring parts.
View details03Performance checks must match the actual function of the part; a generic test cannot represent every braking, sealing, electrical or rotating component.
View details04Pre-shipment inspection confirms that the prepared goods and export pack correspond to the released order, not just that individual parts look acceptable.
View detailsProcess video
Clutch, engine and lamp assembly and testing recorded on site.
Clutch covers are assembled and checked at each workstation.
Clutch discs are tested on automated equipment before packing.
Operators install and check external engine components at the workstation.
Diesel engine assembly at multiple production stations.
A replacement headlamp is powered and checked at the workbench.
Headlamp components are assembled with dedicated production equipment.